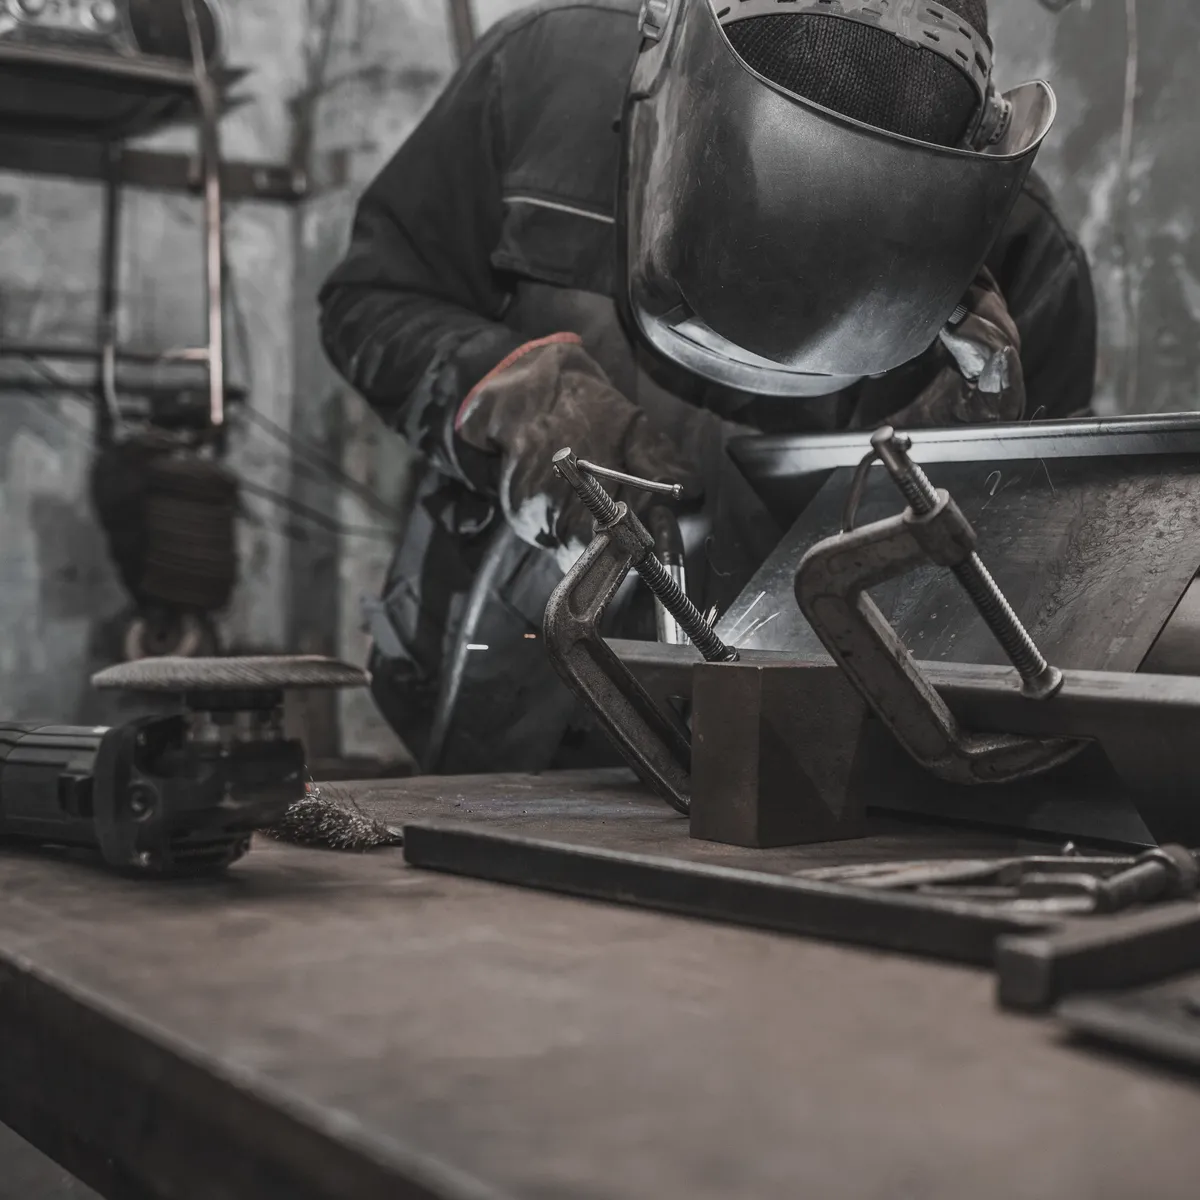
MIG and TIG welding in Hull: which process for which metal
MIG and TIG welding in Hull starts with the metal. MIG gives strength and speed on steel. TIG suits thin sections, visible joints and reactive metals. We back-purge stainless to keep the root clean, then remove the heat tint. Titanium is shielded front and back and checked against the colour scale.
The work we take on needs a clean, controllable process, and MIG and TIG give us that on steel, stainless, aluminium and titanium.
Welding process by material
TIG
For thin sections, stainless, titanium and visible welds.
Hull & East YorkshireMIG
For mild steel, thicker sections and production runs.
Hull & East YorkshireMild steel
Fabrication, repairs and modifications, by MIG or TIG as the job needs.
Hull & East YorkshireStainless
Back-purged for clean root runs. Heat tint removed by pickling or bead blast for food, pharmaceutical and marine use.
Hull & East YorkshireAluminium
AC TIG and pulsed MIG for 5083, 6082 and castings.
Hull & East YorkshireTitanium
Back purge, trailing shield and a chamber for small parts. Weld colour checked against the acceptance scale.
Hull & East YorkshireWelding materials and grades
| Mild steel | General fabrication and repairs |
|---|---|
| Stainless | 304, 316, duplex on request. Purged and finished to specification. |
| Aluminium | 5083, 6082, castings |
| Titanium | Grade 2 and Grade 5 under full inert shielding |
| Dissimilar joints | Stainless to mild steel with 309L filler |
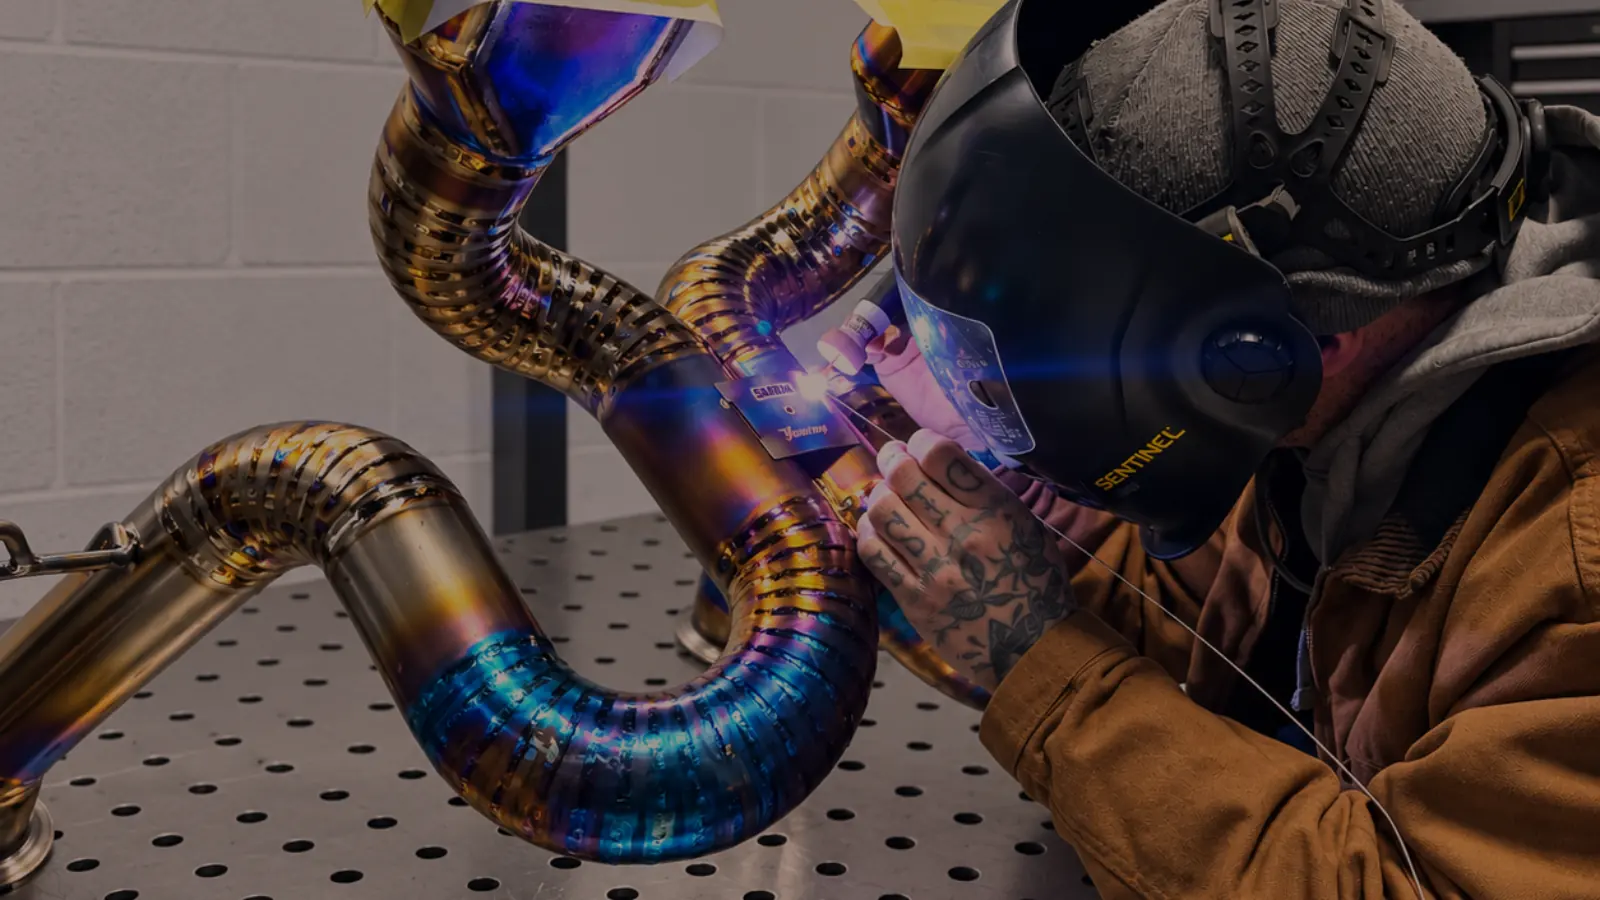
Stainless welds are back-purged and pickled to remove heat tint.
Heat tint left on a stainless weld is where corrosion starts.
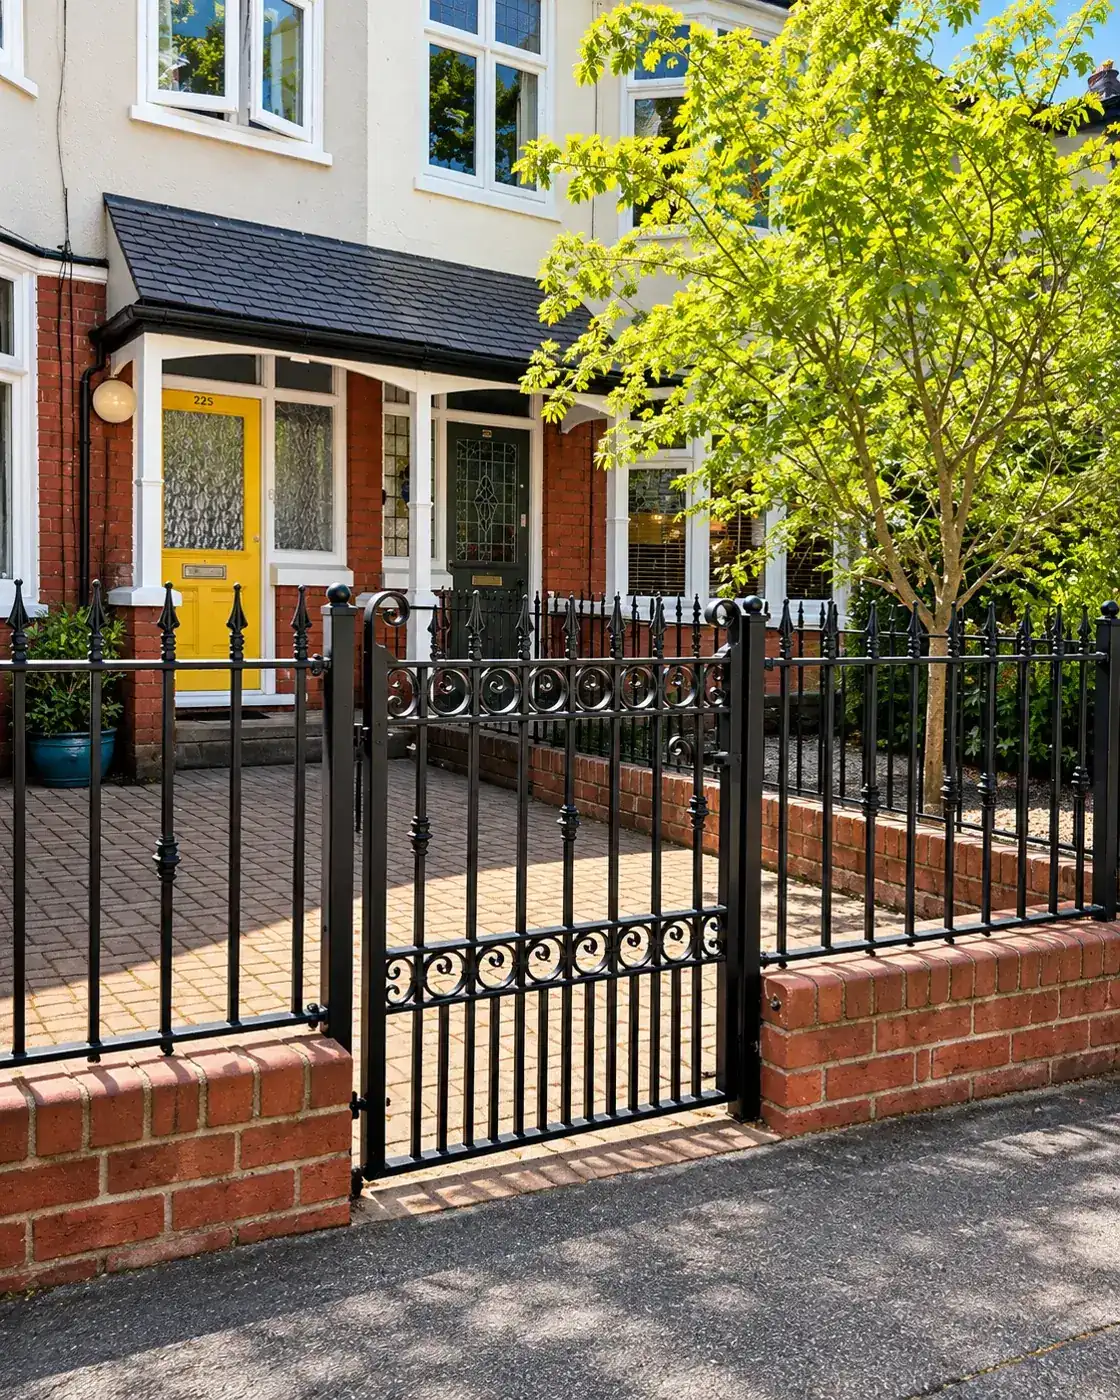
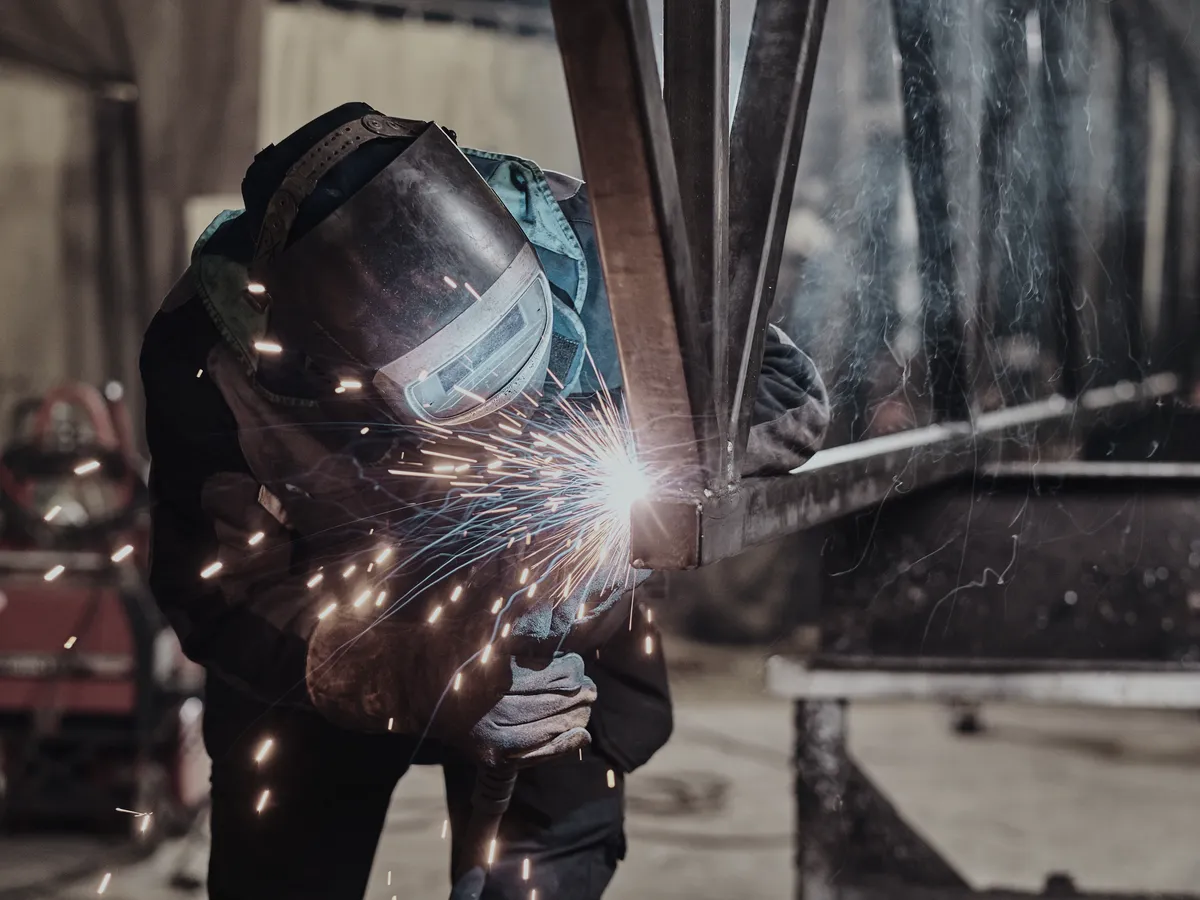
Recent work from our Hull workshop
MIG & TIG welding questions
Not covered here? Call or WhatsApp and ask.
MIG or TIG for my job?
TIG for thin, visible or reactive metals. MIG for strength and speed on steel. We choose and explain why.
Can you weld stainless to mild steel?
Yes, with 309L filler. It is routine for brackets, transitions and repairs.
Can you weld titanium?
Yes. Titanium needs full shielding on both sides of the joint until it cools. The purge, trailing shield and chamber provide that.
Can you weld to a drawing or specification?
Yes. Give us the weld size, material and what the drawing calls for. We work to it, with dressing and inspection to match.
Can you weld brass or cast iron?
Brass, yes, with care over zinc fumes. Cast iron is sometimes repairable with preheat and the right filler. Send a photo.
Can I bring a part to the workshop?
Yes, by appointment. Small parts are often quicker in the workshop than on site. Send a photo first for a price.
Related services
Aluminium welding
Castings, tanks, frames, boat and trailer parts in 5083, 6082 and cast alloys.
Hull & East Yorkshire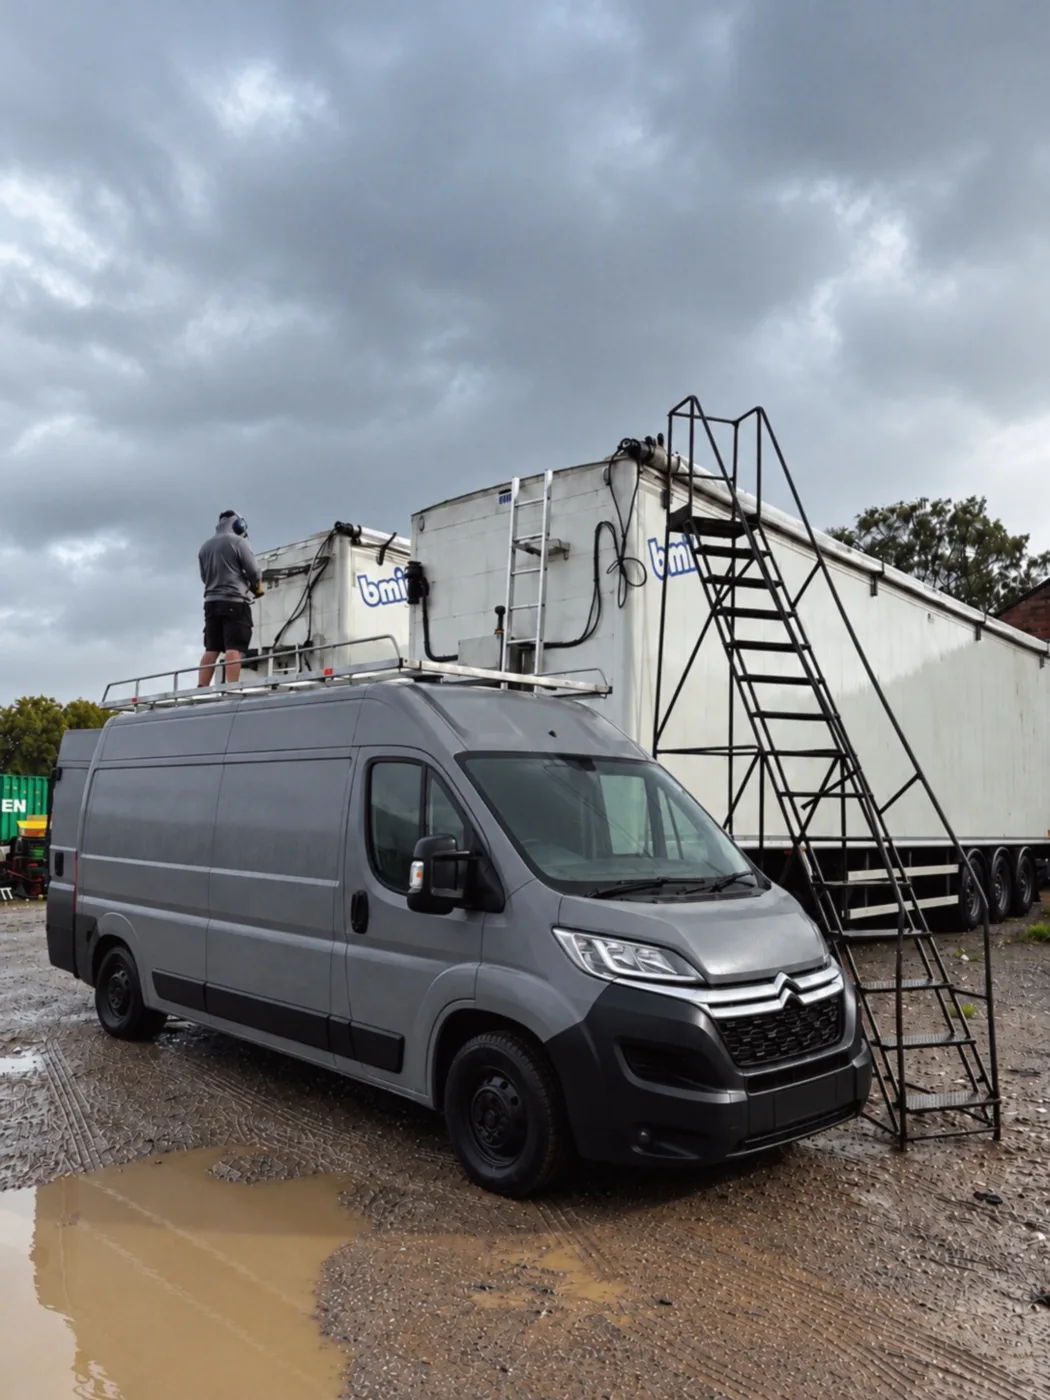
Mobile welding
A welder, a self-powered rig and consumables for steel, stainless, aluminium and titanium, brought to your yard, farm, factory or quayside.
Hull & East Yorkshire
Steel fabrication
Frames, skids, guards, platforms, brackets and one-off parts in mild steel, stainless, aluminium and titanium.
Hull & East YorkshireSite work across Hull, the East Riding and north Lincolnshire, including these towns.
Send a photo or a drawing for a price
WhatsApp 07364 137317 · Call 01482 530020 · info@onmet.uk